A rocket nozzle sees combustion gas running into the thousands of degrees Fahrenheit, moving at multiples of the speed of sound, for the entire length of a motor burn.
No common structural material survives that unprotected.
Metal nozzles get around the problem with cooling – propellant is pumped through channels in the nozzle wall, and the wall never gets hot enough to fail. But that only works if there’s a coolant loop to pump through, and a solid rocket motor doesn’t have one. There’s no propellant flow to route through the nozzle wall, no pump, no plumbing. So solid motor nozzles solve the heat problem differently: they let part of the nozzle burn away, on purpose, in a controlled and predictable way.
That’s the job phenolic composites do. Carbon-phenolic liners protected the nozzle of the Space Shuttle’s Reusable Solid Rocket Motor (RSRM) this way – built from a phenolic resin, carbon cloth, and carbon filler prepreg, tape-wrapped around a mandrel and cured before final machining.
The environment a nozzle has to survive
The throat of a solid rocket motor is one of the harshest places to put a structural material anywhere in aerospace. NASA test data for one solid-propellant motor recorded a calculated flame temperature of 4,700°F2, and heat flux at the internal liner of a solid motor nozzle can run as high as 10 MW/m² during a burn. Add the pressure and velocity of the exhaust gas, chemical attack from combustion products, erosion from condensed particles like alumina in solid propellants, and the thermal-gradient stress of heating a structure that fast, and it’s clear why a nozzle can’t just be a piece of metal.
Liquid engines get around some of this with regenerative cooling – propellant flows through channels in the nozzle wall on its way to the combustor, carrying heat away before it accumulates. It works well, but it needs plumbing, pumps, and a coolant source, none of which a solid motor has. So instead of resisting the heat, phenolic ablative liners are designed to give a little of themselves up to it.
How the material actually protects the nozzle
Phenolic resin on its own isn’t much use here. In nozzle hardware it’s always the matrix in a fiber-reinforced composite. Carbon-phenolic goes in the highest-heat, most erosion-prone zones, usually near the throat. Silica-phenolic shows up where insulation matters more than erosion resistance. Glass-phenolic handles the cooler backing and insulation regions.
What all of them do when they meet hot exhaust is pyrolyze. Rather than melting, the resin breaks down chemically – an endothermic reaction that consumes energy instead of passing it straight through the material. That breakdown leaves behind a carbon-rich char, which happens to be a poor conductor of heat, so it insulates whatever sits behind it. Meanwhile, gases released by pyrolysis push outward through the surface, forming a thin boundary layer that further slows heat transfer from the exhaust stream. The surface recedes as all of this happens, physically carrying heat away with the material it removes.
The resin’s own char yield matters here. Reinforced phenol-formaldehyde resins used in these composites typically retain around 55–60% of their original mass as char once they’ve decomposed at temperatures above roughly 650°C in an inert atmosphere – meaning a little over half the resin stays behind doing insulating work, and the rest is given up as pyrolysis gas.
It comes down to a rough heat balance:
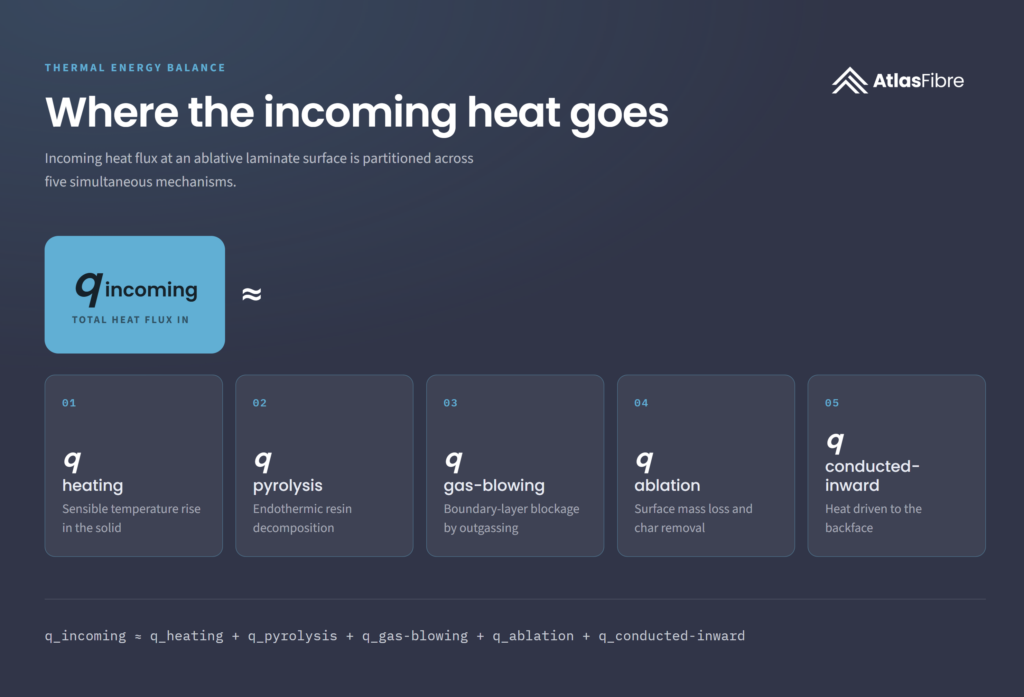


Every term on the right except the last one is heat the ablative process is absorbing or carrying away. The smaller that last term – heat actually conducted into the structure – the better the design is doing its job.
Reinforcement does the structural work
None of this holds together without fiber reinforcement. Carbon, silica, or glass fibers give the composite its mechanical integrity, govern how it erodes, stabilize the char layer as it forms, and let engineers tune the material’s properties by direction instead of treating it as uniform. The RSRM’s nozzle liners were built from a three-component prepreg – phenolic resin, carbon cloth, and carbon filler – tape-wrapped, then hydroclave – or autoclave-cured, and machined to final contour. Fiber orientation, resin content, filler type, density, and tape-wrap angle all shape how the finished part conducts heat, holds its char, releases gas, and erodes. That’s why liner fabrication is treated as a controlled process with engineering behind each parameter, not a generic layup.
A nozzle is rarely one material end to end
Different zones of a nozzle see different severities of heat, so the liner is often graded rather than uniform. The throat gets the highest-performance ablative – usually carbon-phenolic – because it sees the worst combination of gas velocity, heat transfer, and particle impingement. The convergent section just ahead of it still needs a robust ablative composite. Past the throat, in the divergent section, heat flux tends to fall even as surface area grows, which can justify a lighter or more insulating phenolic system. Behind all of it, glass-phenolic, silica-phenolic, or ceramic-fiber/phenolic layers act as insulation and structural backup, keeping heat from reaching the nozzle housing itself.
The tradeoff is built into the design
None of this works if the material is expected to remain unchanged. Phenolic ablatives are chosen precisely because they fail in a way that’s predictable. The engineering problem becomes managing that failure: keeping recession within contour tolerances, keeping the throat from enlarging enough to shift chamber pressure and thrust, keeping the char intact rather than spalling or cracking, keeping the backface temperature below whatever the structural shell, bondline, insulation, or seals behind it can tolerate, and making sure all of that holds for longer than the required burn, with margin.
That combination is why phenolic ablatives show up almost exclusively in hardware meant to fire once – boosters, missiles, launch-vehicle solid motors, sounding rockets, and some liquid-engine combustion-chamber or nozzle liners.
Where it sits against other options
Graphite handles high temperature well and suits small throats, but conducts heat more readily than a phenolic composite and can oxidize or erode depending on the environment. Carbon-carbon manages the most demanding environments of all, at a higher cost and with oxidation protection as a real design concern. Metal with regenerative cooling is durable and can be reused, but it needs a liquid engine’s coolant flow and adds real plumbing complexity. Ceramics handle temperature well but tend to be brittle under thermal shock and mechanical load. Phenolic composites sit in a specific niche – lower cost, low conductivity, structurally useful for a finite burn – in exchange for planned recession and, generally, single use.
The TLDR on Phenolic Nozzles
A rocket nozzle exposed to unprotected combustion gas would fail almost immediately. Phenolic composites solve that by failing on purpose, in a way that’s engineered and predictable: the char layer insulates, pyrolysis absorbs heat before it reaches the structure, and fiber reinforcement holds everything together as the surface recedes. The material is consumed doing its job, which is exactly why it’s built for one well-characterized burn rather than a service life.